DURO-SE – the new high-performance coating
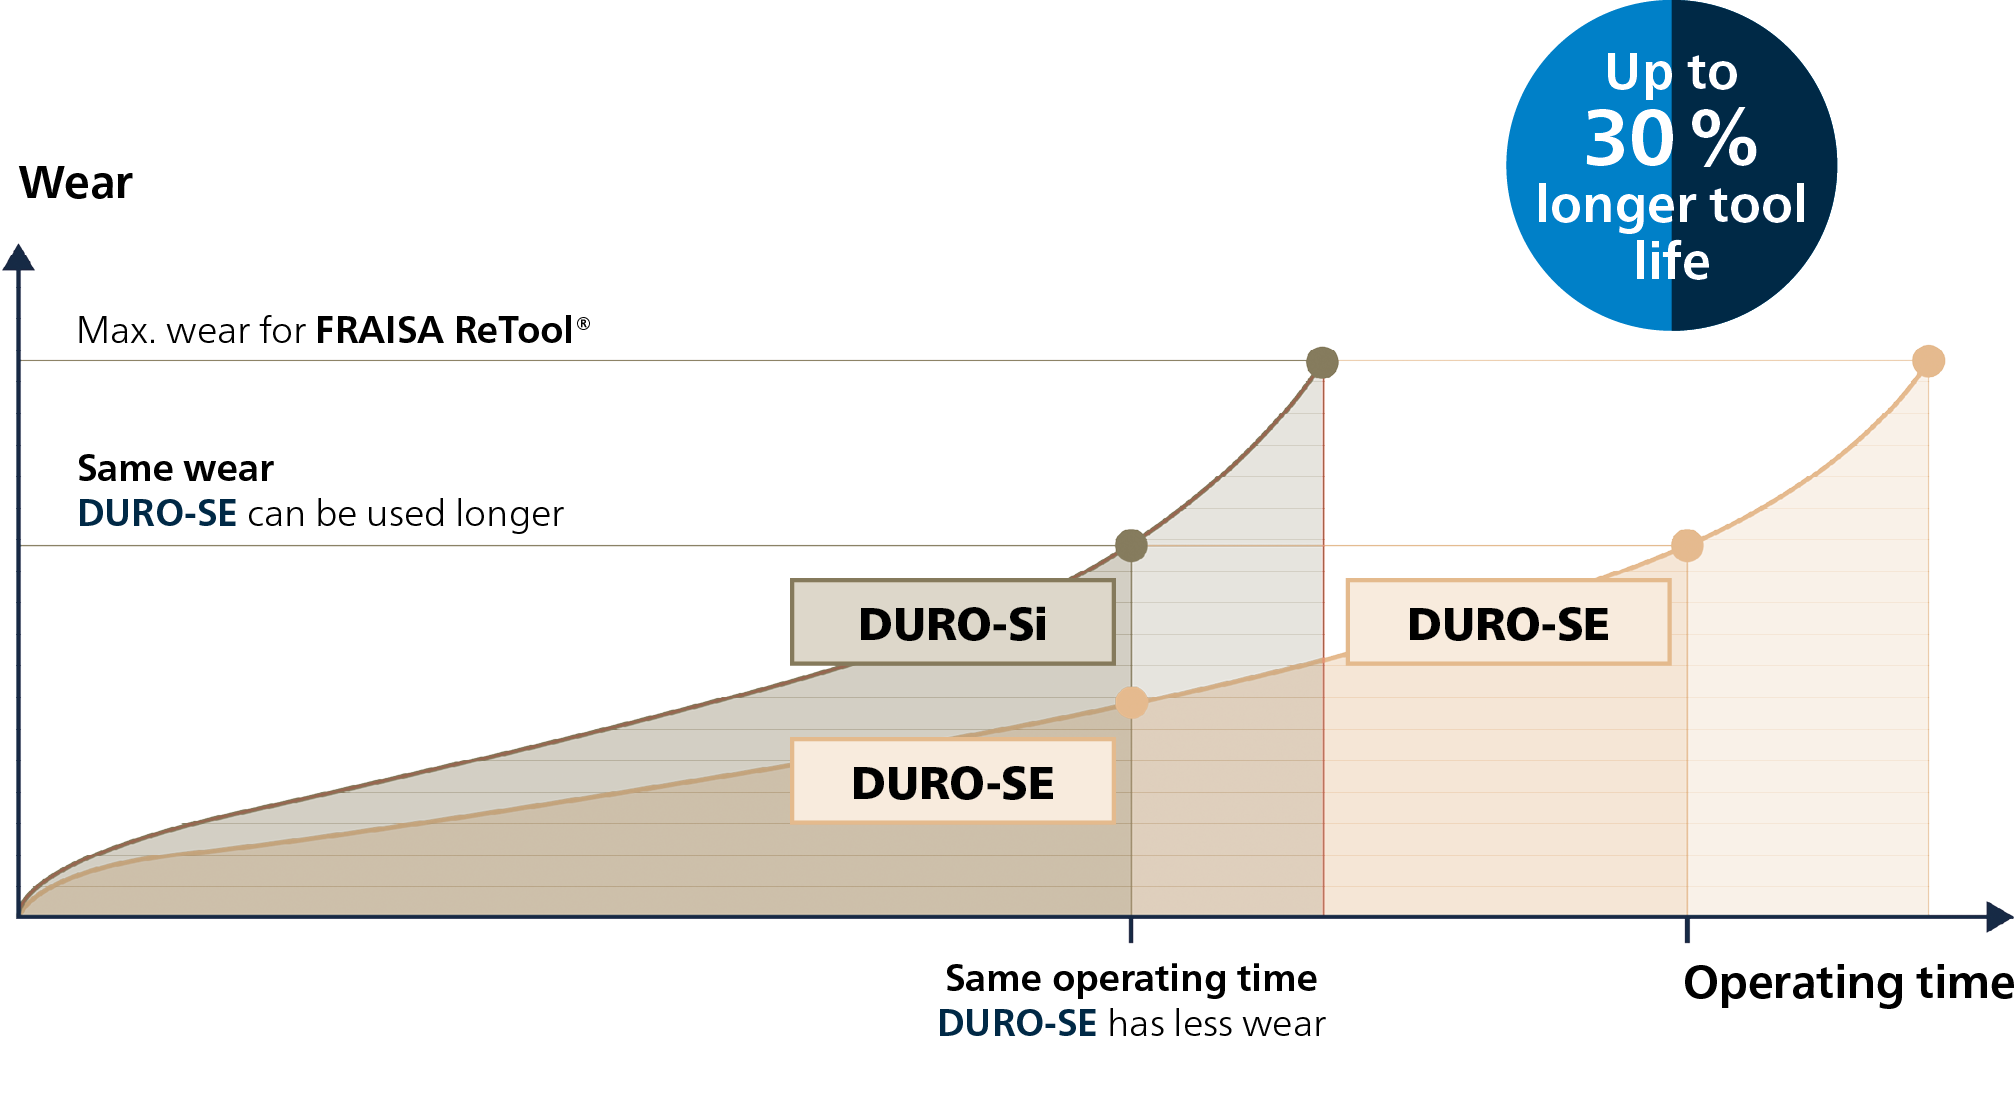
Improved wear resistance for up to 30% longer tool life
Up to 30% longer tool life
Clean surface finishes without rework or scrap
Stable cutting edge, high dimensional accuracy, fully reproducible
Process-reliable – consistent performance and predictable wear
Stainless steel, titanium, nickel alloys, and hardened steels up to 70 HRC
FRAISA ReTool® qualified – reconditionable to 100% original performance
Same tools, new coating – a reliable path to longer tool life
Demanding materials place the highest requirements on process stability, quality and predictable tool life. Stainless steels, titanium, or hardened steels over 55 HRC place heavy demands on tools – faster wear, material adhesion, and hard-to-predict processes lead to unplanned downtime, scrap, and rising unit costs. This quickly becomes an economic risk, especially with complex 3D geometries and tight tolerances.
DURO-SE was developed specifically for these requirements – as the logical next step in the evolution of the proven DURO-Si coating, which is now being phased out, with identical geometry, the same tool families, and unchanged application data. For users who are already working with FRAISA tools and DURO-Si, switching is particularly easy.

What stays the same
- Same geometry
- Same application data
- Same price
- Same tool families
No adjustments. Productive immediately.
Good to know
- DURO-SE is currently available for seven tool families – with more to follow progressively
- Existing DURO-Si inventory remains fully usable without restrictions
- DURO-Si is not being phased out abruptly, but will be gradually replaced by DURO-SE
- Switching involves no extra cost – geometry, application data, and price structure stay identical
- FRAISA ReTool© qualified
Higher performance. Same price. Zero effort to switch.
The process remains the same; the coating changes. And what’s changing is the performance. With up to 30% longer tool life, DURO-SE offers a measurable advantage. The extremely smooth PVD surface reduces friction and heat build-up, prevents built-up edge formation and reliably stabilizes the cutting edge. The result: consistent surface quality and high dimensional accuracy – reproducible throughout the tool's entire life. Less scrap, fewer unplanned tool changes and lower costs per part.
The matching cutting data is available in the FRAISA ToolExpert® – validated and ready for immediate use. Tools with DURO-SE are fully qualified for FRAISA ReTool® – ensuring a closed, sustainable tool cycle.
| Characteristics | DURO-SE advantage |
|---|---|
| Coating material | AlTiSiN-based, optimized composition |
| Price-performance ratio | Same price, longer tool life |
| Wear resistance | Outstanding – significantly longer tool life |
DURO-SE technology – durable under thermal stress, stable at the cutting edge
DURO-SE is an optimized, AlTiSiN-based high-performance coating that combines three key properties. HiPIMS technology combines the advantages of arc and sputtering technologies. This produces a highly dense, uniform coating structure with an extremely smooth surface – reducing friction, minimizing material adhesion, and reliably protecting the cutting edge, even under high thermal loads. The result: maximum tool life, process reliability, and reproducible component quality.
HiPIMS precision – evident in coating structure and surface finish
Predictable wear, plannable tool life
Reliable even at high cutting speeds
Clean surfaces, less rework
 High layer density
The very dense layer structure makes it difficult for microcracks to propagate. The result is uniform, predictable wear and greater process reliability throughout the entire tool life.
 Thermally resilient
DURO-SE is designed to withstand abrasive and thermal stresses. The coating withstands shortterm temperature peaks up to 1,100 °C (process-dependent) – a range where many coatings reach their limits. The substrate remains protected even under demanding conditions.
 Extremely smooth surface
The low-droplet coating surface reduces friction and heat generation. Material adhesion and built-up edges are effectively minimized – for clean surfaces and a stable cutting edge.
Less wear, longer tool life – DURO-SE in a direct comparison
The following wear images show the direct comparison. At identical cutting data and the same operating time, tools with DURO-SE exhibit significantly lower and more uniform wear characteristics. The cutting edge stays intact longer – for measurably longer tool life and consistently high component quality.
Cylindrical end mill SX Ø10 mm
HPC partial cut in 1.4571 | Wear after 61 min operating time
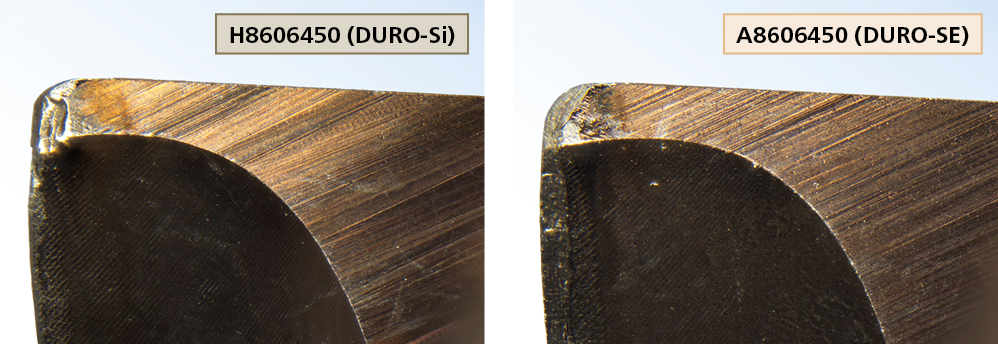
| vc | fz | ap | ae | n | vf | Q |
|---|---|---|---|---|---|---|
| 80 m/min | 0.045 mm | 15 mm | 6.5 mm | 2546 min-1 | 458 mm/min | 44.66 cm3/min |
Cylindrical end mill HX Ø10 mm
HDC-S in 1.2379 (61 HRC) | Wear after 60 min operating time
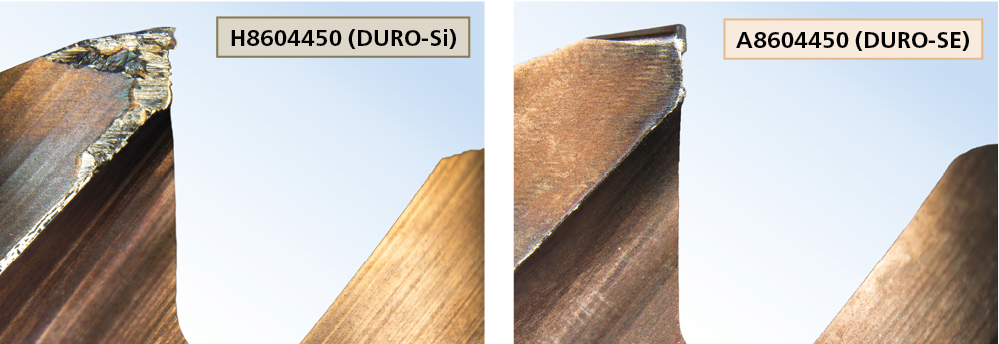
| vc | fz | ap | ae | n | vf | Q |
|---|---|---|---|---|---|---|
| 108 m/min | 0.104 mm | 22 mm | 0.25 mm | 3438 min-1 | 1430 mm/min | 7.87 cm3/min |
High feed end mill XFeed-H Ø3 mm
High feed milling in S390 (67 HRC) | Wear after 29 min operating time
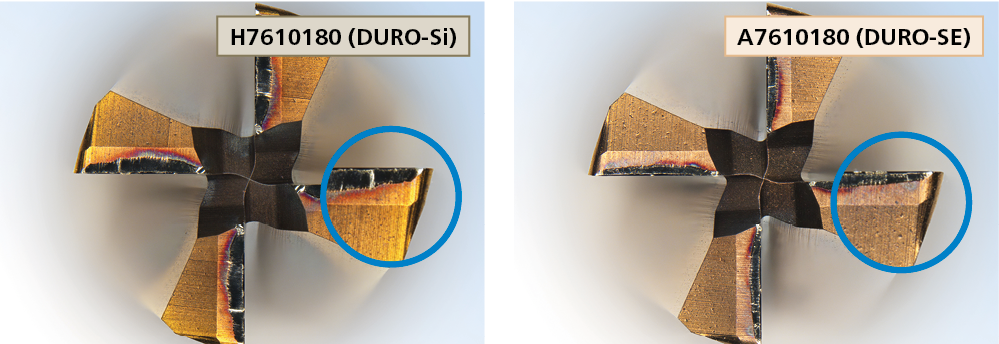
| vc | fz | ap | ae | n | vf | Q |
|---|---|---|---|---|---|---|
| 36 m/min | 0.032 mm | 0.06 mm | 2.25 mm | 3820 min-1 | 489 mm/min | 0.07 cm3/min |
Ball nose end mill SpheroX Ø6 mm
HSC Z-level roughing in 1.2083 (52 HRC) | Wear after 115 min operating time
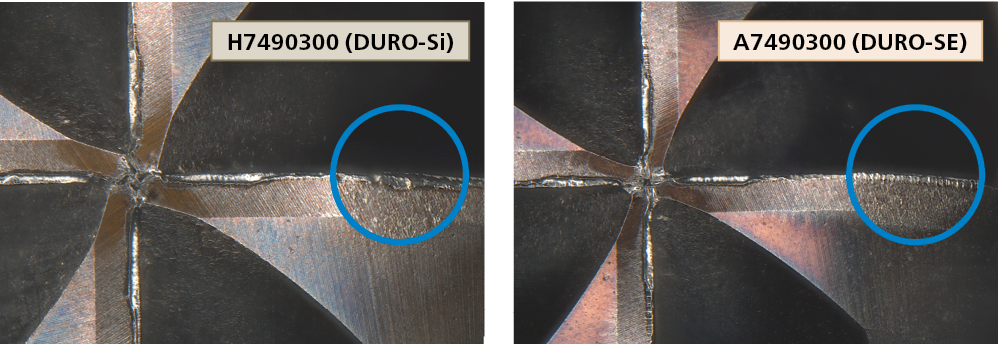
| vc | fz | ap | ae | n | vf | Q |
|---|---|---|---|---|---|---|
| 93 m/min | 0.036 mm | 0.72 mm | 1.2 mm | 7590 min-1 | 1092 mm/min | 0.94 cm3/min |
Corner radius end mill XSpeed-H Ø10 mm
HSC Z-level roughing in 1.2379 (61 HRC) | Wear after 59 min operating time
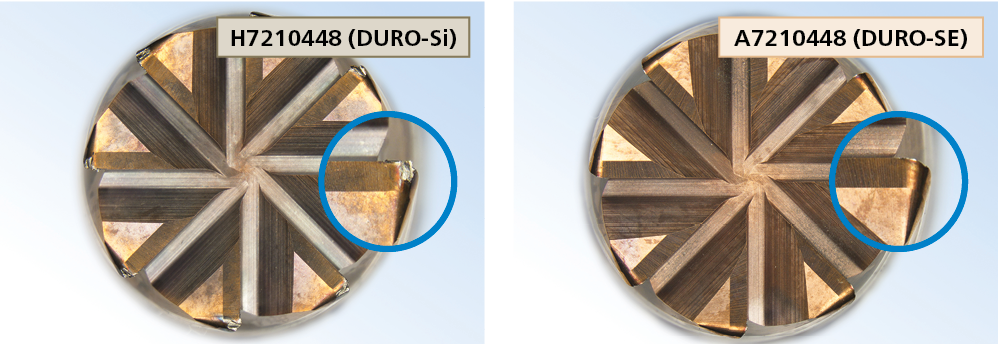
| vc | fz | ap | ae | n | vf | Q |
|---|---|---|---|---|---|---|
| 50 m/min | 0.033 mm | 0.2 mm | 6 mm | 1624 min-1 | 429 mm/min | 0.51 cm3/min |
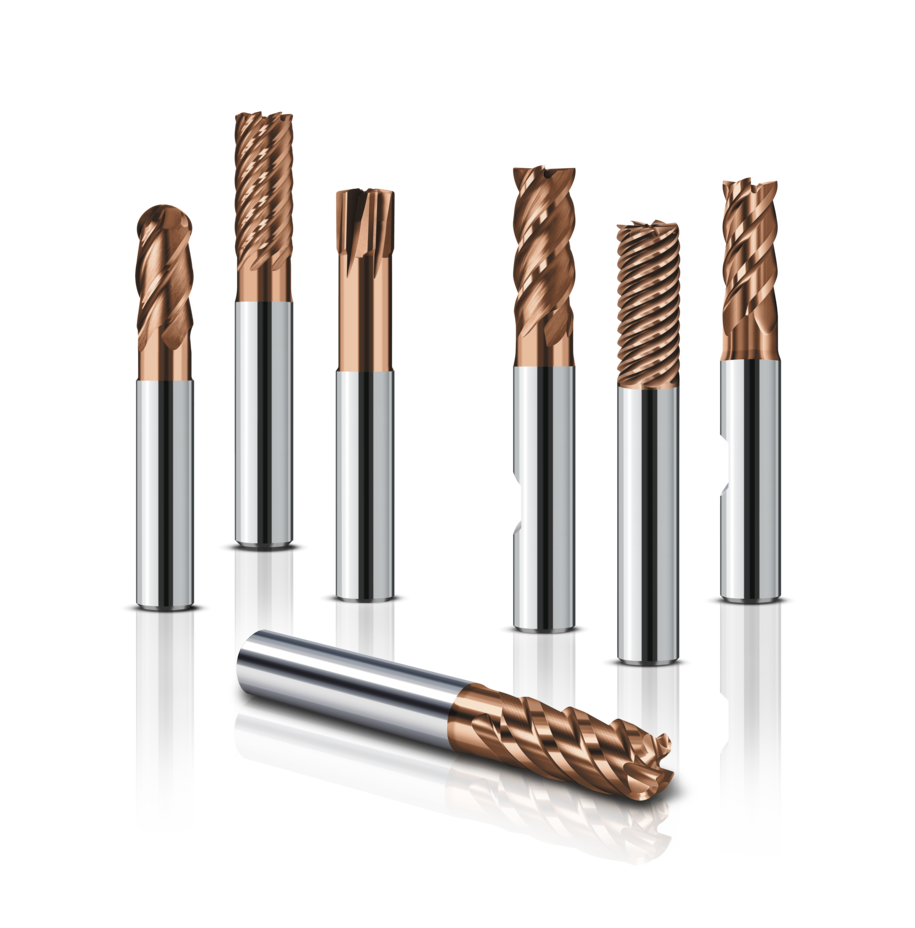
Seven tool families with DURO-SE – the right tool for every application
Whether roughing, finishing, or complex 3D machining – the following tool families cover a broad spectrum of applications and materials. You'll find all articles, diameters, and optimal cutting data in the FRAISA ToolExpert® and the webshop.
Cylindrical end mill HX
short neck (A8504 / A8604)
- Roughing HPC, roughing HDC, finishing
- Hardened steels HRC 48–56, HRC 56–60, HRC > 60, HSS
- d₁ 3–20 mm, 4 cutting edges, 18 items
Cylindrical end mill SX
short neck (A8506 / A8606)
- Roughing HPC, roughing HDC, finishing
- Stainless steel, HRC > 24, titanium, manganese steel, nickel alloys, HSS
- d₁ 3–20 mm, 4 cutting edges, 18 items
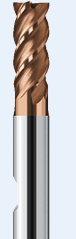
Corner radius end mill HX
short neck (A8507 / A8607)
- Plunging, roughing HPC, roughing HDC, finishing
- Hardened steels HRC 48–56, HRC 56–60, HRC > 60, HSS
- d₁ 3–16 mm, 4 cutting edges, 25 items
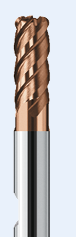
Cylindrical end mill Multicut XF
(A15250)
- Finishing
- Steel, stainless steel, titanium, hardened steels up to HRC > 60, aluminium
- d₁ 3–20 mm, 5/7 cutting edges, 9 items
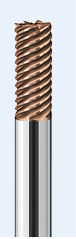
Ball nose end mill SpheroX
3xd neck (A7490)
- Plunging, roughing, roughing HDC, finishing
- Hardened steels HRC 42–48, HRC 48–56, HRC 56–60, HRC > 60, titanium, HSS
- d₁ 1–16 mm, 4 cutting edges, 10 items
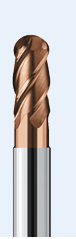
Corner radius end mill XSpeed-H
3xd neck (A7210)
- Roughing HPC, roughing HDC, finishing
- Hardened steels HRC 48–56, HRC 56–60, HRC > 60, HSS
- d₁ 2–12 mm, 6/8 cutting edges, 16 items
High feed end mill XFeed-H
3xd neck (A7610)
- High feed end milling
- Hardened steels HRC 48–56, HRC 56–60, HRC > 60, HSS
- d₁ 1–16 mm, 4/6 cutting edges, 10 items